Calcium Silicate: Our Product Information
As a calcium silicate supplier and distributor, we provide high‑quality material for further processing and for use as a functional component in a wide range of products. Our specialized precipitated synthetic calcium silicate offers exceptionally high absorptive capacity, making it an ideal carrier for delivering liquid materials in powder form or for imparting uniquely absorptive qualities.
Product Specification
Calcium Silicate Powder: Definition and Why It Matters in the Food & Flavor Industry
Calcium silicate powder is widely valued in the Food & Flavor industry for its outstanding anti‑caking, free‑flow, and carrier properties. Thanks to its exceptionally high moisture absorption capacity, it ensures that dry powders remain free‑flowing, stable, and easy to process, even in humid conditions or hygroscopic formulations.
From a material classification perspective, calcium silicate belongs to the group of inorganic silicates and is commonly described as calcium metasilicate, a calcium–silicon oxide compound. Its structure enables strong physical adsorption rather than chemical interaction, which explains its high absorption capacity and inert behavior in food and flavor systems. Unlike reactive silica or cementitious silicate materials, precipitated calcium silicate is engineered for controlled performance, consistent quality, and safe handling. Identified by CAS 1344-95-2, it is widely used where moisture management, carrier functionality, and powder stability are required.
Key Functional Benefits of Calcium Silicate Powder
Calcium silicate delivers multiple performance advantages that make it an essential ingredient across food, flavor, and nutritional applications. Its most important functional benefits include:
-
Excellent anti‑caking performance
-
High absorption of oils, moisture, and liquid ingredients
-
Neutral taste and odor for formulation flexibility
-
Improved powder flowability and extended shelf life
-
High efficiency at very low inclusion levels
These properties make calcium silicate an ideal choice whenever stability, flowability, or moisture control are required.
Ideal Applications for Calcium Silicate in Food and Flavor Manufacturing
Calcium silicate powder is used throughout the Food & Flavor industry in a variety of dry ingredients, flavor systems, and functional blends. Its performance benefits make it suitable for the following applications:
1. Dry Food Ingredients (Anti‑Caking Agent)
Due to its strong moisture absorption capabilities, calcium silicate keeps powders loose and free‑flowing, even in humid environments or hygroscopic systems.
2. Flavor & Fragrance Powders (Carrier / Flow Aid)
Commonly used as a carrier for liquid flavors, aroma compounds, and fragrance oils, it enables the conversion of liquids into easy‑to‑handle powders.
3. Sweeteners & Sugar Blends
Calcium silicate helps control hygroscopicity in high‑sugar systems, supporting stable texture and preventing clumping.
4. Nutritional & Functional Food Powders
Its neutral sensory profile makes it ideal for nutritional blends, where it provides stability without affecting taste or aroma, even at low use levels.
5. Dairy & Dairy‑Analog Powders
In fat‑containing powders such as creamers or dairy analogs, calcium silicate improves flowability, handling, and consistency.
6. Dry Beverage Mixes
By improving flow and preventing clumping, calcium silicate ensures consistent dosing, processing efficiency, and reliable solubility in beverage formulations.
Summary --- Why Calcium Silicate Is Essential for Free‑Flowing, Stable Powder Systems
Calcium silicate is a highly efficient ingredient for dry, hygroscopic, or oil‑containing powders, offering superior benefits in flowability, moisture management, stability, and processing efficiency. Its multifunctional performance makes it a staple across the food, flavor, beverage, and nutritional industries---helping manufacturers maintain high product quality and optimized production processes.
 XylitolCAS-Nr.87-99-0SynonymSweeteners / Sugar replacements
 Acacia GumCAS-Nr.9000-01-5SynonymGum arabic, arabic gum
 Acesulfame KCAS-Nr.55589-62-3SynonymAce K
 Agave SyrupCAS-Nr.-SynonymAgave
 Ascorbic AcidCAS-Nr.50-81-7SynonymVitamin C
 CaffeineCAS-Nr.58-08-2SynonymEnergy Ingredients
 Calcium SilicateCAS-Nr.1344-95-2SynonymCalcium silicon oxide, Calcium metasilicate
 Citric AcidCAS-Nr.77-92-9SynonymCAA
 DextroseCAS-Nr.1496309SynonymGlucose
 ErythritolCAS-Nr.149-32-6SynonymSweeteners / Sugar replacements
- GlycineCAS-Nr.56-40-6SynonymAminoacetic Acid
 L-CysteineCAS-Nr.52-90-4SynonymThioserin
 L-LysineCAS-Nr.657-27-2Synonym2,6-Diaminohexanoic Acid
 L-ThreonineCAS-Nr.72-19-5SynonymL-2-Amino-3-Hydroxybutyric Acid
 Magnesium CitrateCAS-Nr.7779-25-1SynonymAcidifiers / Acidity Regulators
 MaltitolCAS-Nr.585-88-6SynonymSweeteners / Sugar replacements
 Microcrystalline CelluloseCAS-Nr.9004-34-6SynonymCELLULOSE MICROCRYSTALLINE;Α-Cellulose
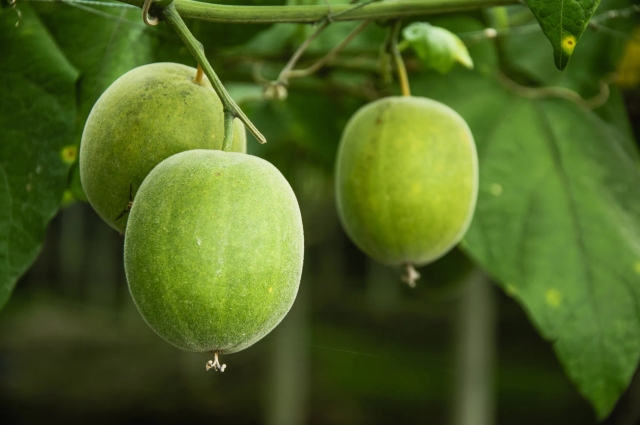 Monk FruitCAS-Nr.-SynonymLuo Han Guo
 NatamycinCAS-Nr.7681-93-8SynonymPimaricin
 Potassium SorbateCAS-Nr.24634-61-5SynonymPreservatives
 Potato StarchCAS-Nr.9005-25-8SynonymProtein / Starches
 Sodium AscorbateCAS-Nr.134-03-2SynonymSodascorbate
 Sodium DiacetateCAS-Nr.126-96-5SynonymSDA
 Sorbitol Crystalline PowderCAS-Nr.50-70-4SynonymD-Glucitol
 SucraloseCAS-Nr.56038-13-2SynonymTrichlorosucrose
 Tapioca StarchCAS-Nr.900-25-8SynonymProtein / Starches
 TaurineCAS-Nr.107-35-7Synonym2-Aminoethanesulfonic Acid
 Tripotassium CitrateCAS-Nr.866-84-2SynonymTPC
 Trisodium CitrateCAS-Nr.6132-04-3SynonymTSC
 VanillinCAS-Nr.121-33-5SynonymFlavors
 Xanthan GumCAS-Nr.11138-66-2SynonymXanthan
- XylitolCAS-Nr.87-99-0SynonymSweeteners / Sugar replacements
- Acacia GumCAS-Nr.9000-01-5SynonymGum arabic, arabic gum

128 South Tryon Street, Suite 1580 Charlotte,
NC 28202, USA
Jebsen & Jessen Life Science USA is part of the Jebsen & Jessen Hamburg Group


